Manual Case Packing vs All-in-one Case Packers: Which Solution Is Better for Modern Manufacturing?
Release time: 2026-07-24
Table of Contents
Introduction
As manufacturing industries continue to pursue higher efficiency and more stable production, packaging processes have become an important factor affecting overall productivity. Many companies still rely on manual case packing, especially in small-scale production environments. However, with increasing labor costs, stricter quality requirements, and growing production demands, traditional manual operations are facing more challenges.
For manufacturers looking for a more efficient packaging solution, All-in-one Case Packers provide an integrated approach that combines automation, accuracy, and flexibility. As an experienced packaging equipment supplier, HRS Seelong Machinery provides advanced cartoning and case packing solutions designed to help companies improve packaging performance and adapt to modern production requirements.

The Challenges of Manual Case Packing in Modern Production
Manual case packing has been widely used because of its simple operation and low initial investment. Workers can adjust packing methods according to different product types, which provides flexibility for small-batch production.
However, as production volume increases, manual operations may create several limitations. Packing speed often depends on individual workers, making output consistency difficult to maintain. Differences in worker experience can also lead to variations in carton arrangement, loading accuracy, and final packaging quality.
In industries such as pharmaceuticals, food, and consumer goods, where packaging consistency is closely related to product safety and brand image, relying only on manual packing may increase management pressure and quality control costs.
How Do All-in-one Case Packers Improve Packaging Efficiency?
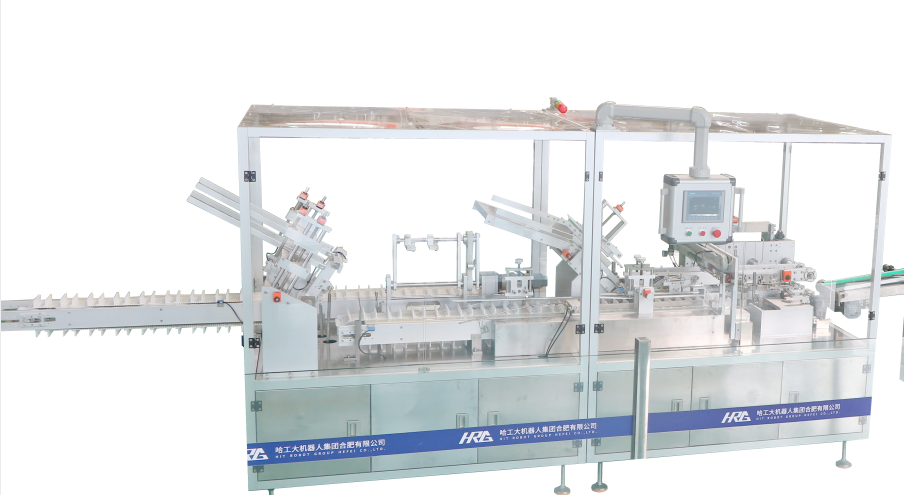
Compared with traditional manual operations, an All-in-one Case Packers system integrates multiple packaging procedures into one automated process. It can complete product loading, case forming, and sealing operations with less manual intervention, helping manufacturers achieve more stable production performance.
The main advantages of automated case packing include improved consistency and better production control. Once parameters are properly configured, the equipment can maintain a stable packing process and reduce errors caused by human operation. This is especially valuable for manufacturers that require continuous production and uniform packaging results.
| Comparison Aspect | Manual Case Packing | All-in-one Case Packers |
| Labor requirement | Requires continuous manual operation | Reduces dependence on manual labor |
| Packing consistency | May vary between operators | Maintains stable packaging quality |
| Production efficiency | Limited by worker speed | Supports continuous automated production |
| Long-term expansion | Difficult to increase capacity | Easier to integrate into automated lines |
Why Are Automated Case Packers Suitable for Growing Manufacturing Companies?
For companies planning long-term production expansion, choosing suitable packaging equipment is not only about improving current efficiency but also preparing for future requirements.
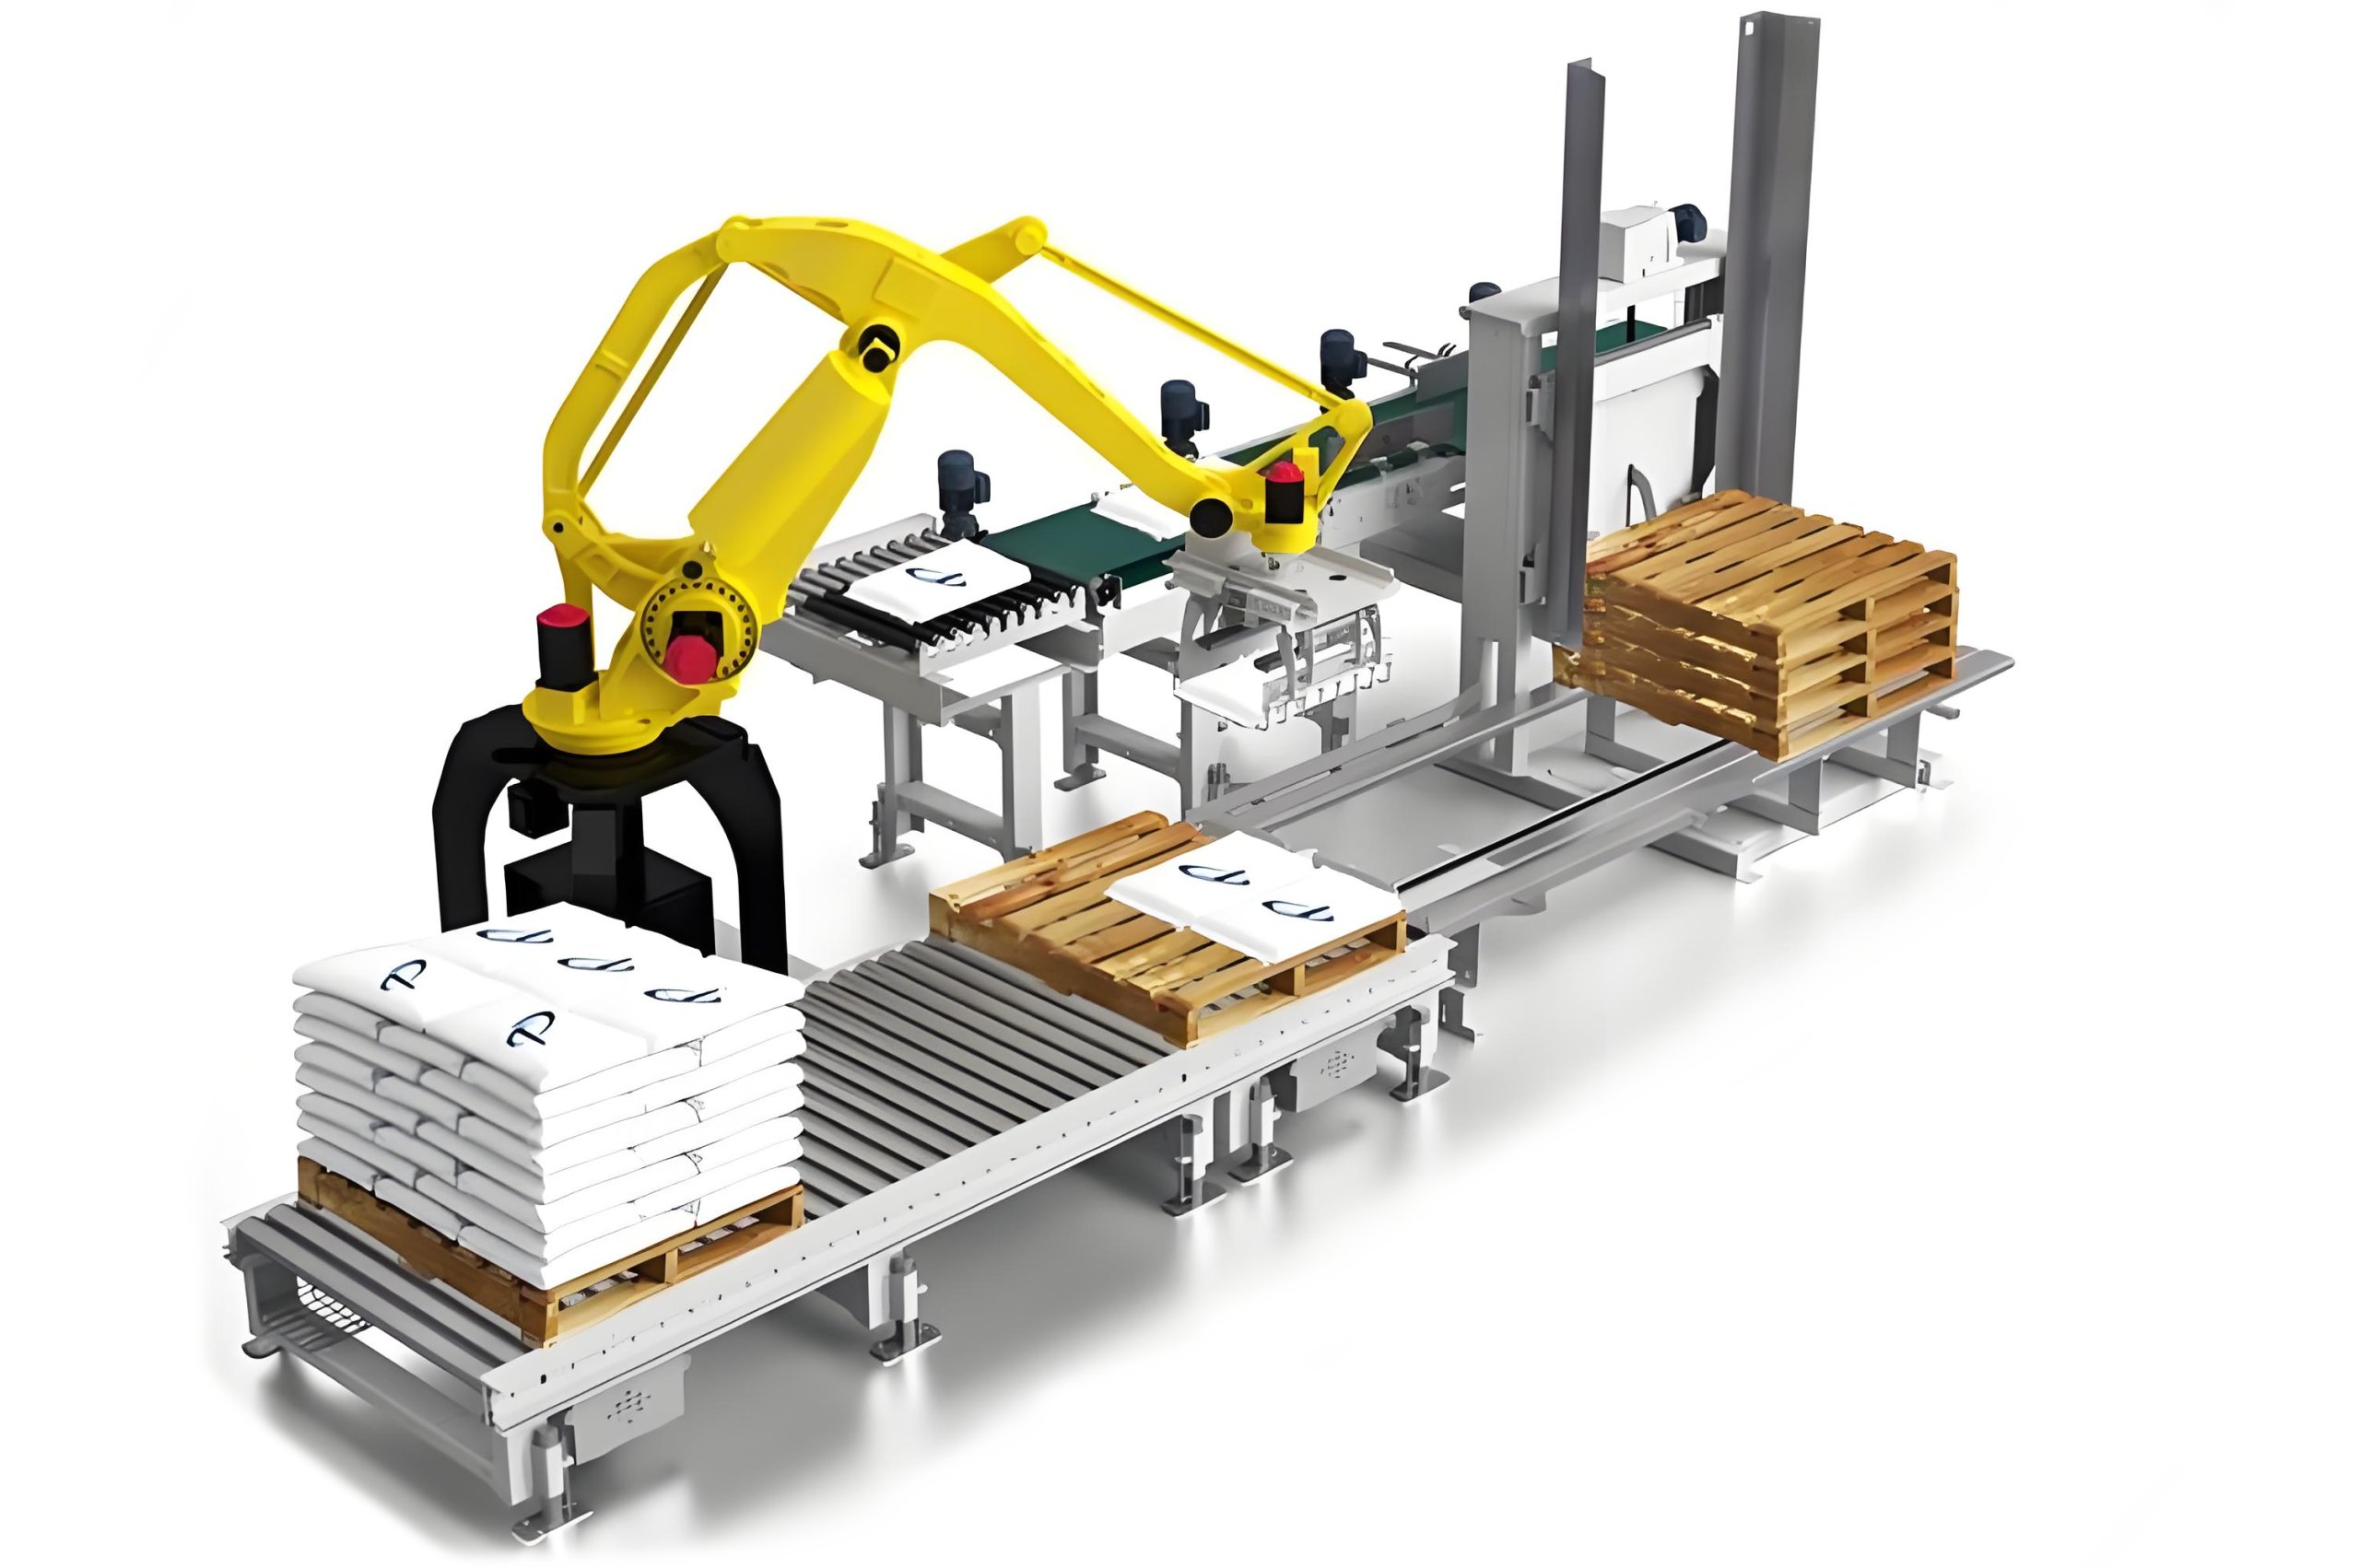
An Automatic Case Packer can work as part of a complete automated packaging system, allowing manufacturers to connect different production stages more smoothly. When production capacity increases, automated equipment can reduce the need for additional labor while maintaining consistent output.
In addition, modern packaging equipment is designed with easier operation and maintenance in mind. Operators can adjust production parameters according to different product specifications, while advanced control systems help monitor the packaging process and improve reliability.
Applications of All-in-one Case Packers in Different Industries
The demand for automated case packing solutions continues to grow across various industries. Pharmaceutical manufacturers use automated packaging systems to improve accuracy and meet strict quality standards. Food and beverage companies rely on stable packing processes to handle high-volume production. Consumer goods manufacturers also benefit from automation when dealing with diversified products and faster market demands.
By combining flexibility with efficient operation, Automated Packaging Machine help manufacturers achieve better productivity while reducing the limitations of traditional packing methods.
Choosing the Right Packaging Solution for Future Production
The choice between manual packing and automated equipment depends on production scale, product type, and business goals. Manual packing may still be suitable for small-volume operations, but companies requiring higher efficiency and consistent quality may find automated solutions more beneficial.
With professional experience in packaging machinery development, HRS Seelong Machinery offers different solutions, including cartoning equipment and integrated packaging systems, to meet the needs of various industries. By selecting the right equipment, manufacturers can improve production stability and build a more efficient packaging process.
FAQ
What is an All-in-one Case Packer?
An All-in-one Case Packer is an automated packaging machine that combines multiple case packing processes, such as carton forming, product loading, and sealing, into one integrated system.
Are automated case packers better than manual packing?
For high-volume production, automated case packers usually provide better consistency, higher efficiency, and lower labor dependence compared with manual packing.
Can case packers be integrated with other packaging equipment?
Yes. Many automated case packing systems can be connected with other packaging equipment, such as cartoners and blister packaging machines, to create a complete packaging line.